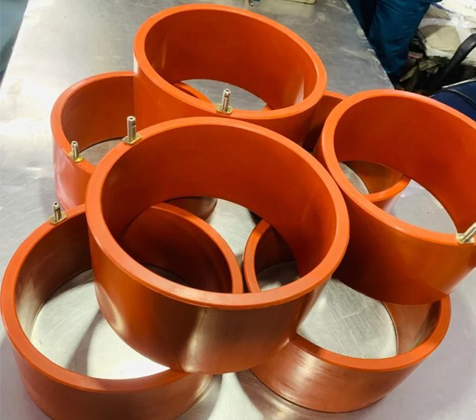
Inflatable Gasket for Big Bag
Dust-Tight Inflatable Sealing for Bulk Bag Discharge & Filling Stations
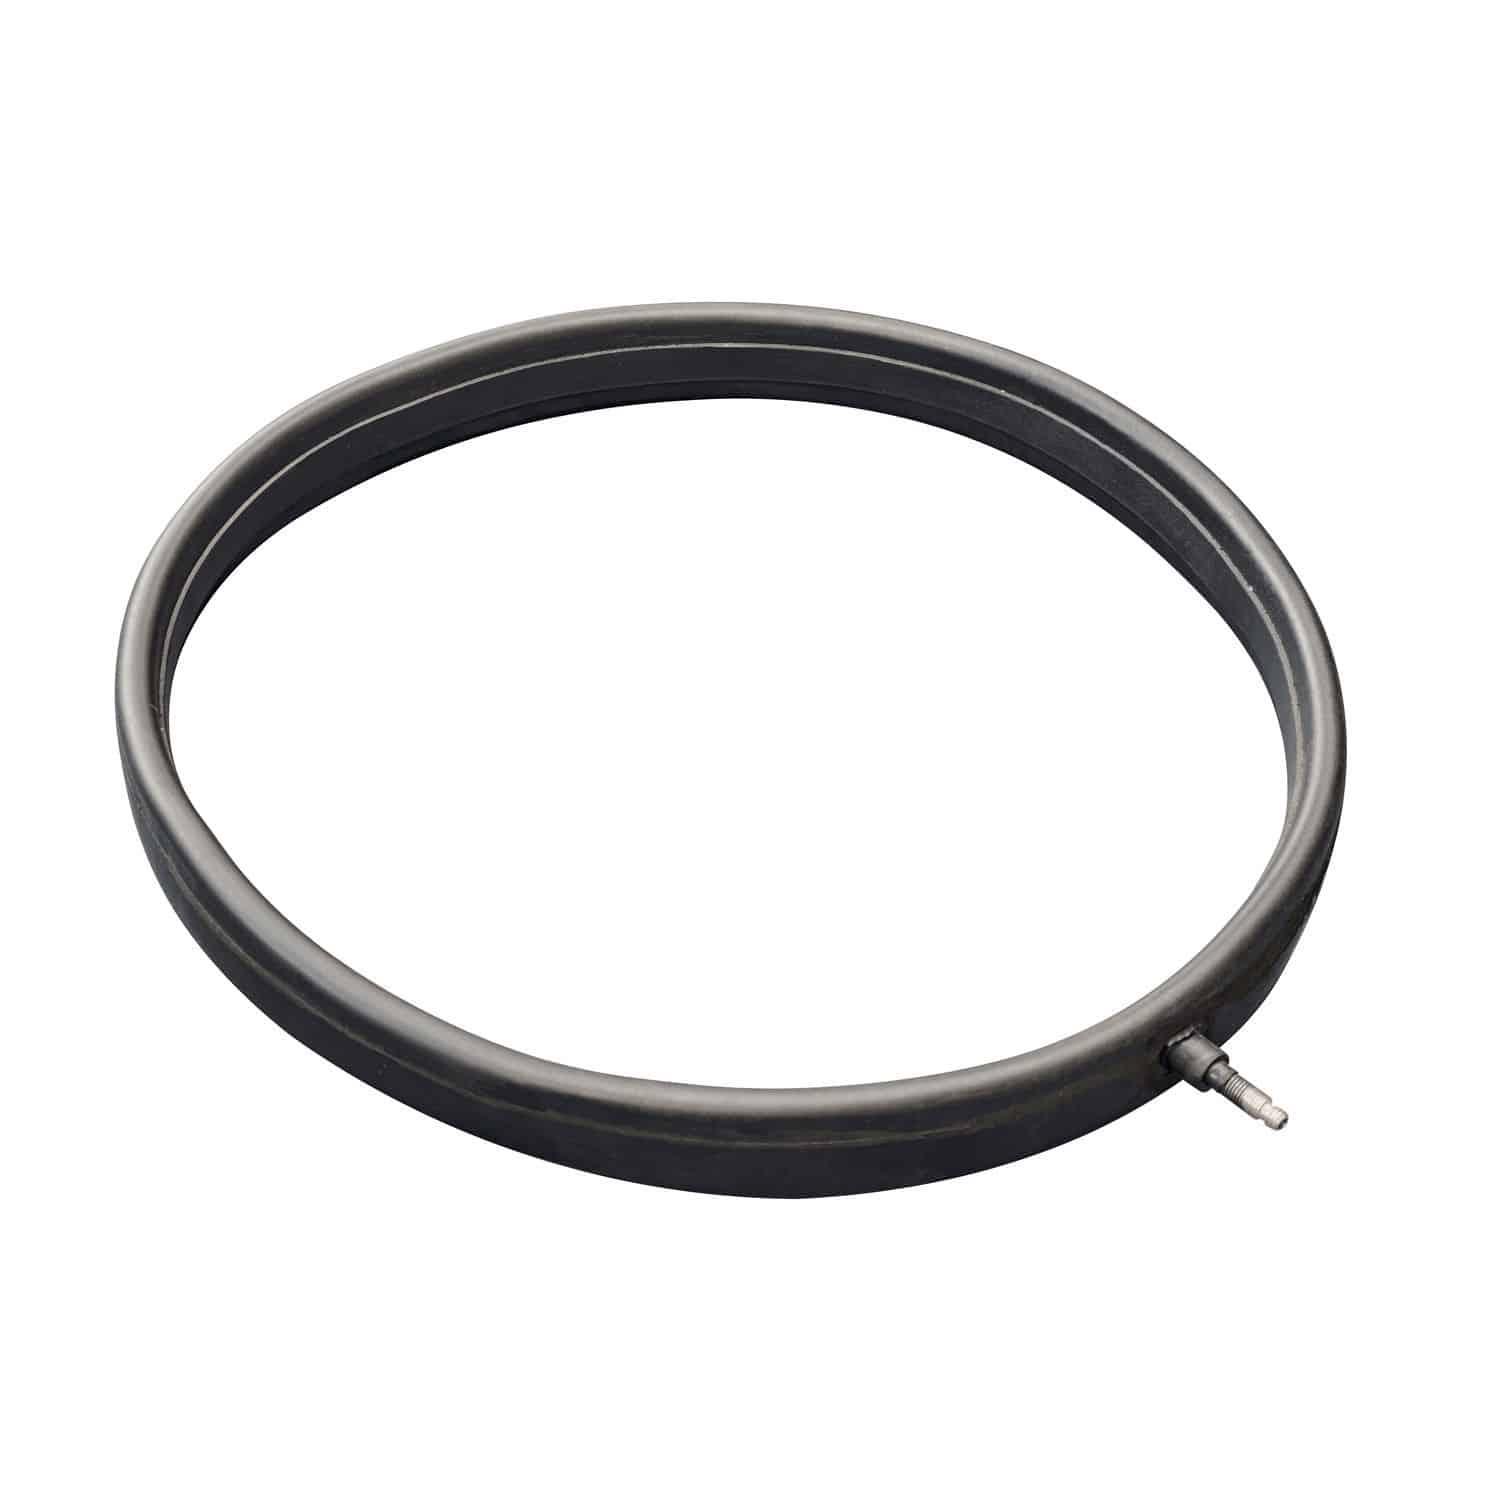
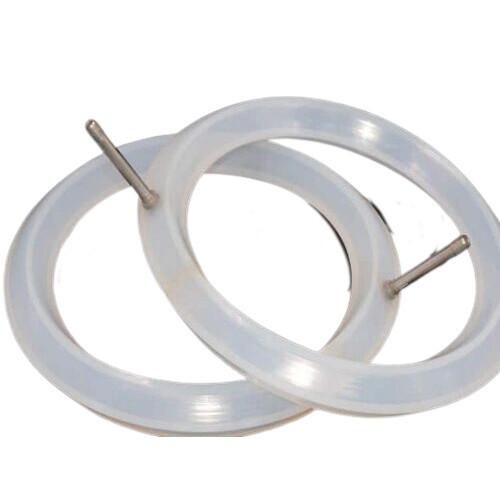
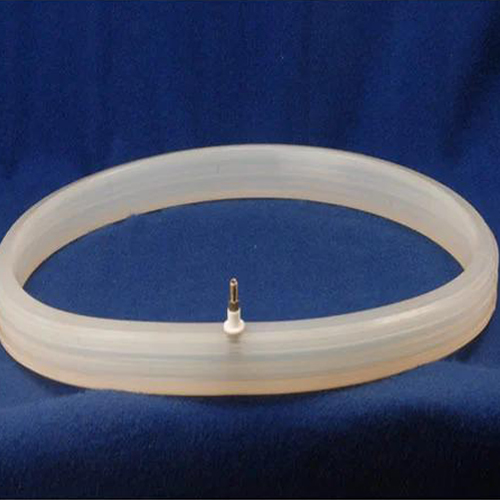
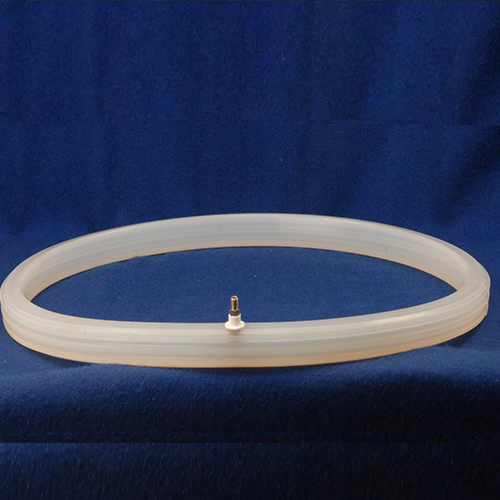
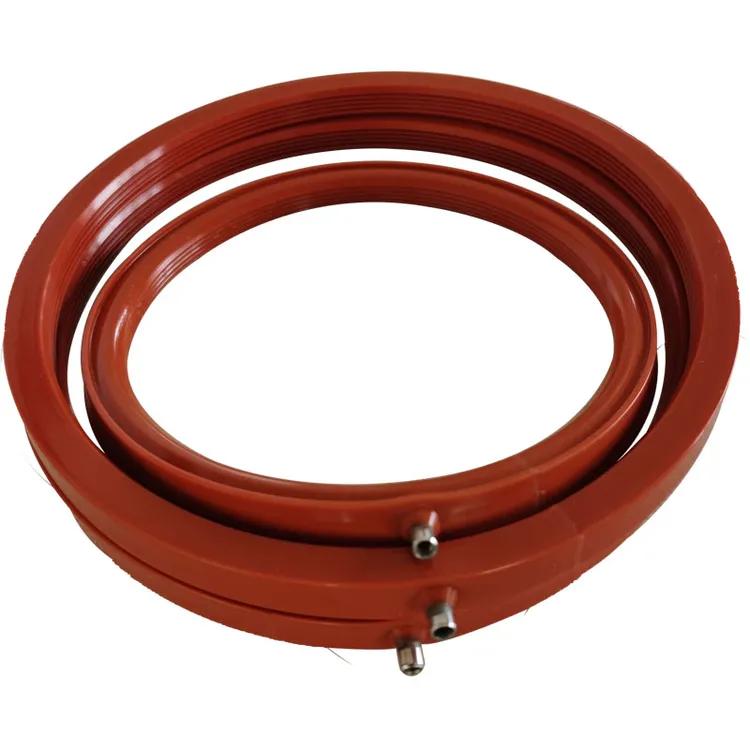
A dust-tight, air-inflated seal that locks a bulk bag spout to its discharge or filling station, keeping powders in and contamination out. Manufactured by Bombay Rubber & Carbon Works.
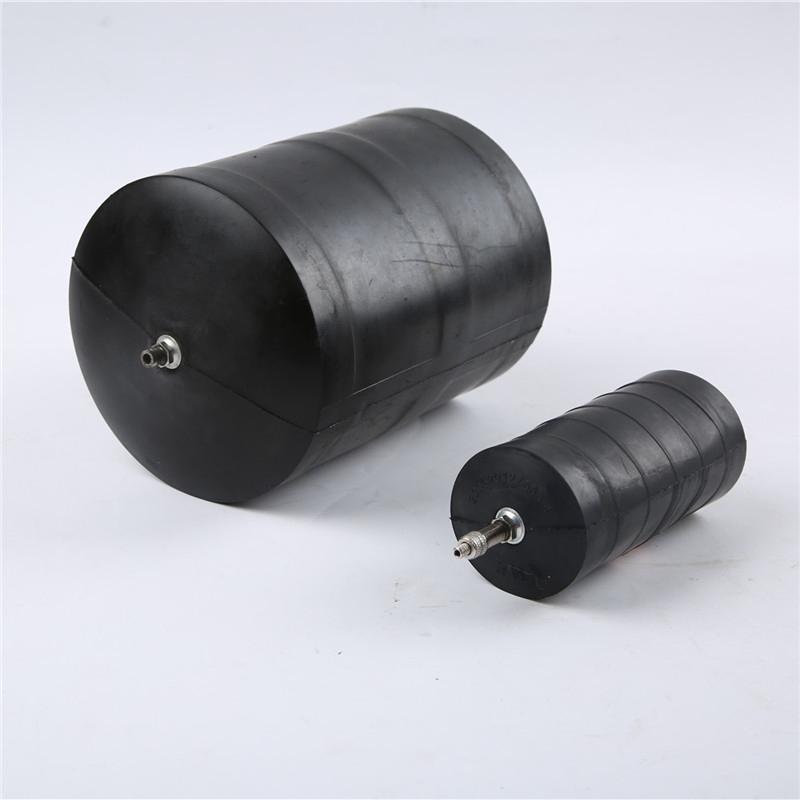
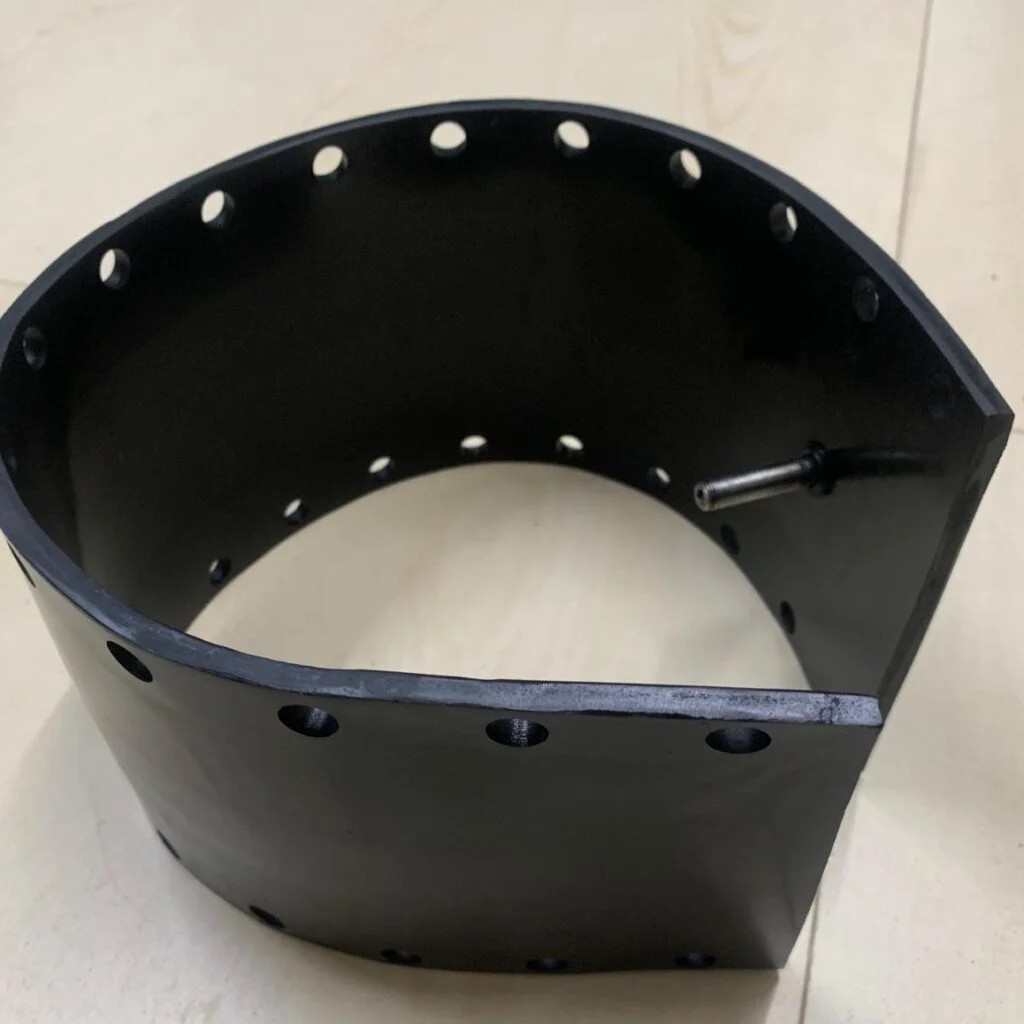
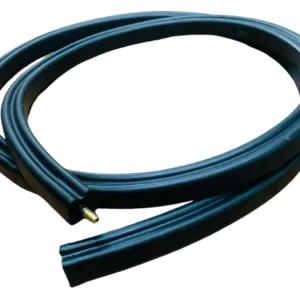
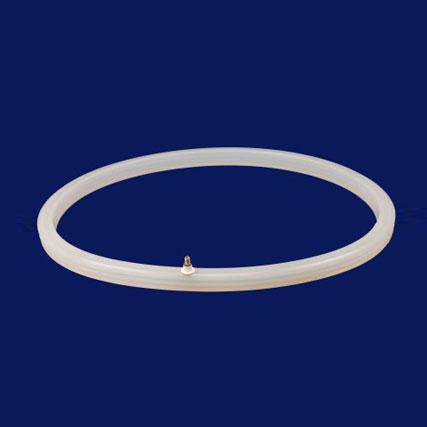
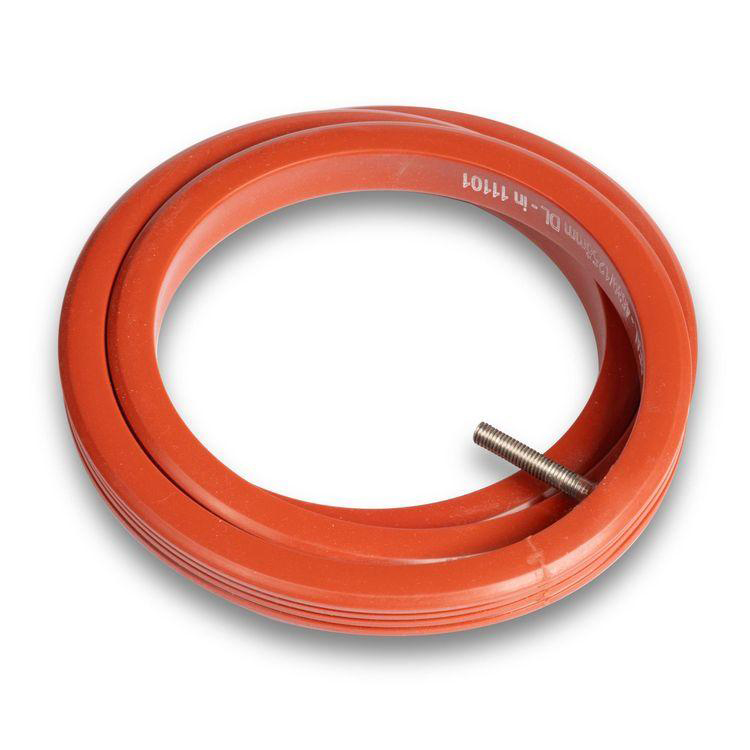
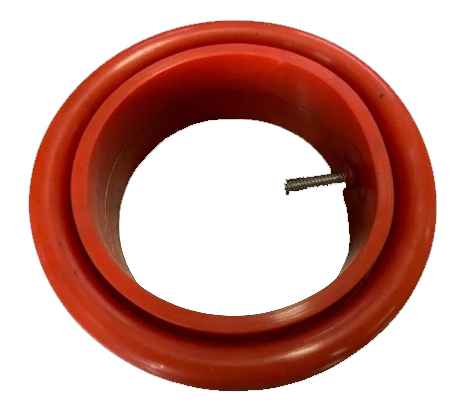
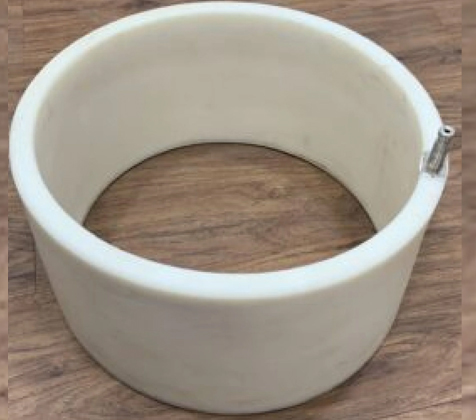
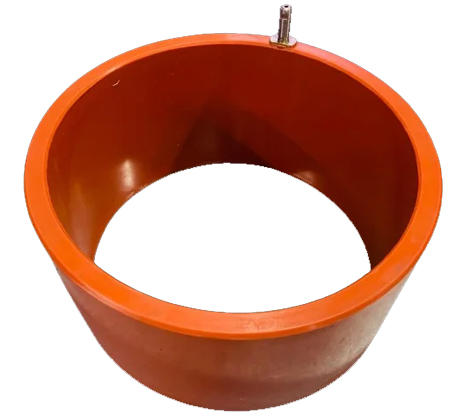
When bulk bags (FIBCs or big bags) are filled or emptied, the connection between the bag spout and the process equipment is the most common point of product leakage. An inflatable gasket solves this by expanding with a small amount of compressed air to grip the spout and the collar, forming a tight, flexible seal. Once the air is released, the gasket relaxes and the bag can be removed quickly and cleanly.
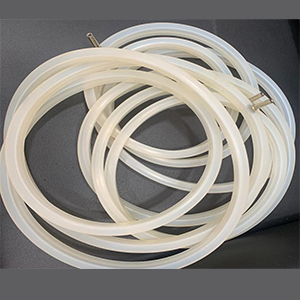
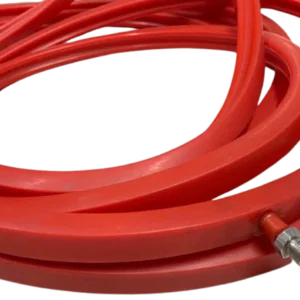
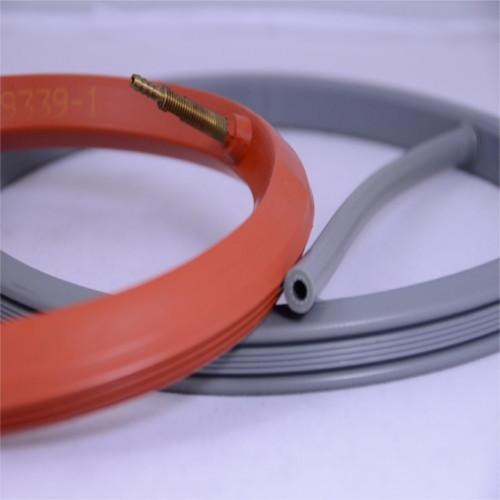
Bombay Rubber & Carbon Works manufactures inflatable gaskets for big bag stations in a choice of food-compatible and industrial rubber materials, made to the diameter and profile of your equipment.
| Parameter | Details |
|---|---|
| Product | Inflatable gasket / bellow seal for bulk bag stations |
| Materials | Silicone (including food grade), natural rubber, polyurethane; neoprene or NBR on request |
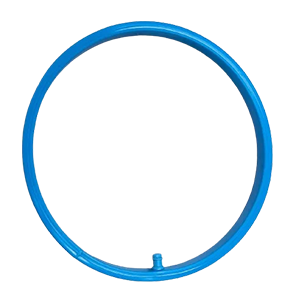
| Shape | Ring or custom profile to suit the docking collar |
| Operating medium | Compressed air through a moulded or fitted inlet |
| Size | Made to your diameter and cross-section |
| Customisation | Size, material, hardness, inlet type and colour as per drawing or sample |
Please confirm working pressure, temperature range and any food or pharma compliance requirements with our team before ordering.
- Dust-tight sealing: helps keep fine powders contained, protecting operators and the working area.
- Fast, clean changeovers: inflate to seal, deflate to release – no clamps or manual tightening.
- Hygienic material options: silicone and other grades suitable for food, pharma and chemical use.
- Flexible fit: tolerates small variations in spout size and alignment.
- Durable construction: designed to withstand repeated inflation cycles.
- Custom made: sizes, profiles and air inlets built to your drawing or sample.
Benefits to Your Plant
- Less product loss and lower housekeeping effort.
- Improved operator safety and cleaner working conditions.
- Quicker bag changes, so higher throughput.
- Better protection of product from outside contamination.
Applications
- Bulk bag discharge and filling stations in powder-handling plants.
- Food and ingredient processing: flour, sugar, starch, spices, additives.
- Pharmaceutical and nutraceutical powder transfer.
- Chemicals, pigments, minerals and polymer powders.
- Containment and dust-control systems for hoppers, feeders and mixers.